
The bottom line
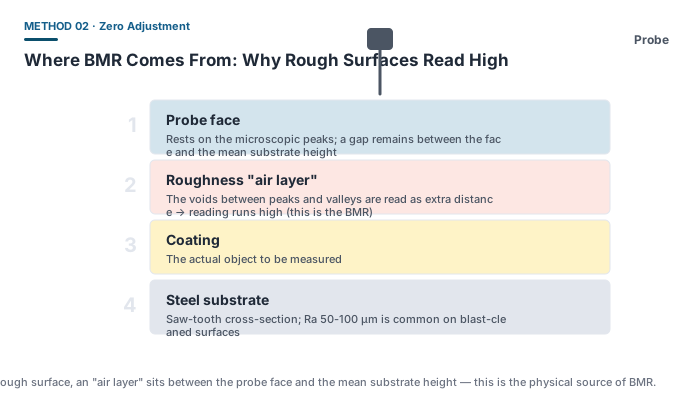
On rough bare steel, the gauge reads a non-zero number — that number is the base metal reading (BMR). If you do not subtract it, your measured thickness includes a layer of “air” that does not exist.
Where BMR comes from
| Source | Mechanism |
|---|---|
| Surface roughness | The probe rests on the peaks; a gap to the mean substrate height creates false thickness |
| Substrate material | Different steel grades have different permeability and conductivity, shifting the gauge baseline |
| Geometry | A curved surface stops the probe face from fully seating; convex surfaces read high |
| Surface state | Scale, oil and dust affect coupling and the magnetic circuit |
What the standards require
- SSPC-PA 2-2022: requires operation per ASTM D7091, which includes the step of adjusting on bare substrate;
- ISO 19840:2012: specifically covers measurement and acceptance of coatings on rough surfaces, requiring correction against substrate of the same roughness;
- ASTM D7091-22: defines Adjustment as zero correction on bare substrate plus shim correction.
Procedure
- Select an uncoated area of the workpiece, or a same-material test piece in identical condition;
- Clean the area, removing scale, oil and dust;
- Take multiple readings there (5-10 recommended) and use the arithmetic mean as the BMR;
- Use the gauge zero-adjustment function to zero the reading, or record the BMR for later subtraction;
- Measure the coating on the painted area; the reading is now the net value after BMR removal;
- Note the BMR value, number of points and adjustment method in the record.
No uncoated area available
On in-service equipment or fully coated workpieces you often cannot find bare substrate. Available alternatives:
- Prepare a test piece of the same material and surface treatment as the part, and leave an uncoated patch as the reference before coating;
- If the workpiece has masked areas (e.g. flange faces, uncoated spots near welds), use them directly for BMR measurement;
- Use the reference plate supplied with the gauge, but note its roughness may differ from the actual workpiece, limiting the correction effect.
Records and reports
BMR is a key intermediate quantity in measurement. The acceptance record should show: the BMR value, the measurement location, the number of points, the shim number used (if slope correction was done) and the adjustment time. This lets a later review reconstruct the measurement condition.
Common misconceptions
- ❌ “The part is freshly made, no correction needed” — a fresh blast-cleaned surface is exactly the most typical source of BMR.
- ❌ “Just reuse last time’s BMR value” — change the workpiece or the steel batch and the BMR can change.
- ❌ “The roughness is small, ignore it” — on a blast-cleaned surface at Ra 50-100 μm, the uncorrected deviation is enough to sway an 80/20 decision.