
The bottom line
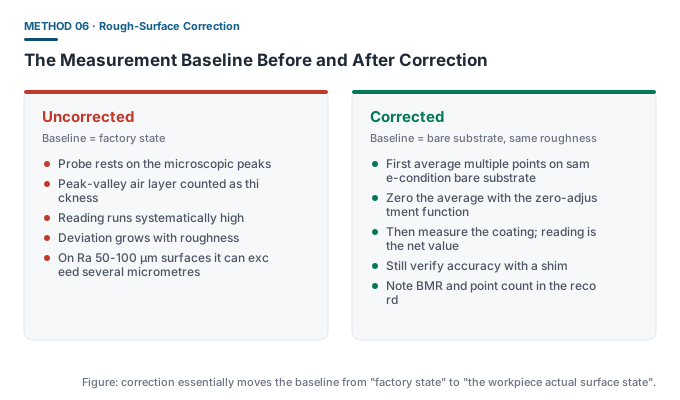
Rough-surface correction is not “subtract a number from the reading”; it is redefining the gauge zero onto the current workpiece surface state. That is also why BMR must be measured, not copied.
Which surfaces count as rough
| Surface type | Source of roughness | Correction needed |
|---|---|---|
| Blast-/shot-blasted steel | Peak-valley structure from abrasive impact; Ra 50-100 μm common | Required |
| Hot-dip galvanised parts | Spangle, zinc nodules and uneven coating surface | Recommended |
| Cast iron parts | As-cast surface and sand pits | Recommended |
| Concrete surface | Exposed aggregate and formwork texture | Watch contact stability for ultrasonic |
| Ordinary cold-rolled steel | Relatively flat surface | Zero adjustment improves consistency |
Procedure
- Select an uncoated area of the workpiece, or a same-material test piece in identical condition;
- Clean the surface, removing rust, scale, oil and loose particles;
- Take 5-10 readings there and compute the arithmetic mean;
- Use the gauge zero-adjustment function to zero the reading (or record the mean for later subtraction);
- Measure on the coated area;
- Verify the corrected accuracy with a shim;
- Note the correction method, BMR value and point count in the record.
Details that go wrong easily
- Baseline must match the workpiece process: using a smooth test piece for a blasted part is no correction at all;
- Baseline must be dry and clean: oil and water change coupling or the magnetic circuit and distort the BMR;
- Correct each steel batch separately: material and surface-treatment differences shift the BMR;
- Still verify after correction: zero adjustment fixes the baseline, but slope correctness must be confirmed with a shim.
Differences between the standards
| Standard | Treatment of rough surfaces |
|---|---|
| ISO 19840:2012 | Specifically sets measurement and acceptance criteria for rough-surface coatings, including roughness correction and a thickness ceiling |
| SSPC-PA 2-2022 | Achieved by referencing the ASTM D7091 Adjustment step; Appendix 5 covers thin coatings after blast cleaning |
| ASTM D7091-22 | Defines Adjustment as “zero correction on bare substrate + shim correction” |
Impact on the acceptance decision
Skipping correction on a rough surface systematically over-states the thickness. In the 80/20 judgement that means:
- The mean can be falsely high, hiding genuinely thin areas;
- Zones that actually fail may be judged pass;
- Different inspectors reach opposite conclusions because of different correction methods, causing disputes.
So correction is not just an operating detail; it is the precondition for a credible conclusion.
Common misconceptions
- ❌ “Just subtract an experience-based value for roughness” — roughness varies widely between processes; it must be measured.
- ❌ “One correction covers the whole project” — different steel batches and surface treatments need separate corrections.
- ❌ “No shim verification after correction” — zero adjustment and slope verification are two different things.