
The bottom line
Faced with an “inaccurate” reading, ask one question first: is it systematic bias or random scatter? The former needs correction; the latter needs more readings. Get the type wrong and the remedy is wrong.
Two classes first: bias and scatter
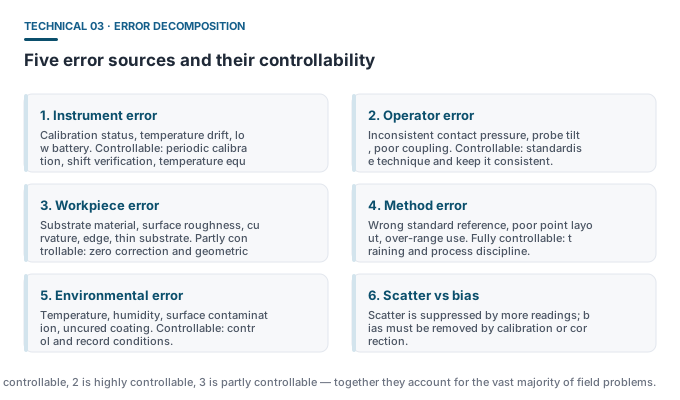
| Feature | Bias (systematic error) | Scatter (random error) |
|---|---|---|
| Behavior | Reading consistently high or low | Readings jump up and down at the same spot |
| Source | Substrate material, roughness, curvature, instrument calibration drift | Contact condition, electronic noise, local non-uniformity |
| Handling | Zero correction, reference-foil adjustment, recalibration | Take more readings and average |
| Removable by averaging? | No | Yes |
The five error sources
1. Instrument error
- Calibration status lapsed (no periodic recalibration, no recheck after impact);
- Temperature drift (no wait for equilibrium after large temperature swing);
- Low battery causing unstable excitation;
- Probe ageing or face wear.
2. Operator error
- Inconsistent probe pressure — affects contact for magnetic/eddy current, coupling-layer thickness for ultrasonic;
- Probe not held perpendicular — especially on small parts and curved surfaces;
- Probe slides during reading — breaks stable contact;
- Wrong or uneven amount of ultrasonic couplant.
3. Workpiece error
- Substrate material differences — permeability of steel grades, conductivity of aluminium alloys vary;
- Surface roughness — a blasted surface lifts the probe, reading runs high;
- Curvature — convex reads high, concave reads low;
- Edge effect — reading changes sharply with position;
- Thin substrate — the field penetrates to the back face, reading runs low.
4. Method error (most controllable)
- Wrong standard reference (using a steel-substrate standard on a non-metallic substrate);
- Poor point layout (clustered in convenient spots, insufficient number of points);
- Using a single reading instead of the point average;
- Over-range use;
- Measuring on an uncured coating.
5. Environmental error
- Temperature change affects instrument and sound velocity;
- Humidity and condensation affect contact conditions;
- Moisture content of concrete and wood changes sound velocity;
- Surface contamination (oil, water, dust, release agent).
Troubleshooting order
- Clean the surface again and re-seat the probe (rule out contact issues);
- Verify instrument status with a reference foil (rule out instrument drift);
- Check whether zero correction was done (rule out substrate and roughness bias);
- Check workpiece geometry (curvature, edge, thickness);
- Check settings (sound velocity, range, unit);
- Only then consider sending it for repair.
How to lower overall uncertainty
- Make the operation a procedure: fixed pressure, fixed angle, fixed number of readings;
- Record the conditions: ambient temperature, surface state, correction method;
- Institutionalise verification: once at the start and once at the end of each shift;
- Group geometrically special spots separately, do not mix them into routine statistics.
Common misconceptions
- “Taking more readings averages out the deviation” — averaging only suppresses random scatter, not systematic bias.
- “The error mainly comes from the instrument” — in field statistics, operator and method errors far outweigh the instrument itself.
- “The accuracy in the manual is my actual accuracy” — that is a design figure under ideal conditions; the real result also depends on the workpiece and the operator.