
The bottom line
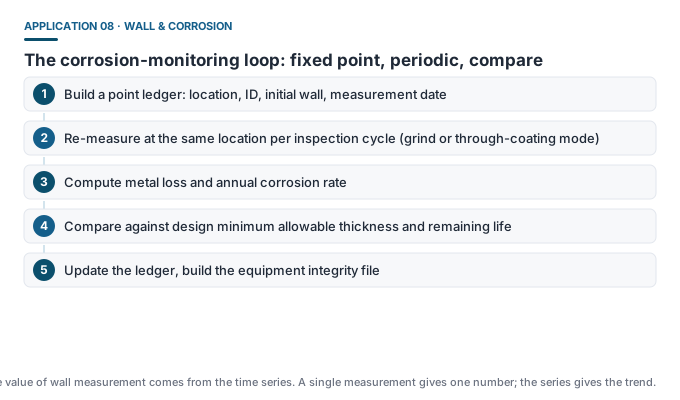
The core of wall measurement is not “how many millimetres” but the difference between two readings at the same location at different times. So the point must be repeatably located, and the record must be complete.
Why ultrasonic
- Non-destructive: no cutting, disassembly or damage to the equipment body;
- Single-side access: only the outer wall is needed, fit for pipes and tanks with only one side reachable;
- Range coverage: metal walls are usually a few to tens of millimetres, exactly the best band of a portable UT gauge;
- Portable: feasible for on-site movement and working at height.
Standards and range
| Model | Range (steel) | Accuracy | Fit |
|---|---|---|---|
| DR83A | 0.9-300 mm | +/- (1%H+0.1) mm | General pipes and vessels |
| DR85A | 0.85-400 mm | +/- (1%H+0.1) mm | General purpose, thicker walls |
| DR86A | 0.55-500 mm | +/- (0.5%H+0.05) mm | High accuracy wide range, thin and thick walls |
| DR87A | 0.55-500 mm (through 3-30 mm) | +/- (0.5%H+0.05) mm | Painted pipes, no-grind measurement |
| DR89S | 0.15-300 mm | +/- (0.01+0.3%H) mm (15P6 std) | Ultra-thin walls and high accuracy |
Six field-operation points
- Surface prep: remove rust scale, oxide, grit and loose coating to expose dense metal;
- Couplant choice: water- or oil-based for normal horizontal surfaces, high-viscosity for vertical and overhead, high-temperature couplant for hot work;
- Sound velocity calibration: back-calculate velocity from a known-thickness block of the same material; do not trust the default;
- Point location: record position (distance from weld, clock angle, height), mark if needed, so the next cycle returns to the same spot;
- Multiple readings: at least 3 readings at one point, watch scatter to judge coupling quality;
- Anomaly check: a low reading first suggests poor coupling or internal scale, before calling it metal loss.
Coated and insulated areas
Anti-corrosion and insulation layers make the normal UT mode count the coating thickness too. Two ways to handle it:
- Through-coating (Echo-Echo) mode: no grinding, measure the substrate wall directly, e.g. Dongru DR87A (through mode 3-30 mm);
- Local grind then measure: the most direct reading, but breaks the coating and needs repair after; fit for a few key points.
Corrosion mapping
For heavily or unevenly thinned equipment, the industry practice is to measure densely over a grid area and plot wall values as a 2D distribution map, showing corrosion hot spots directly. This is the advanced use of UT thickness in industrial inspection, also relying on the same portable gauge and disciplined records.
Common misconceptions
- “One measurement is enough” — only series data give corrosion rate and remaining life.
- “A small reading means corrosion” — internal scale, poor coupling and probe wear all lower the reading; check first.
- “Hot equipment can use a normal probe” — heat damages the probe and changes couplant behaviour; high-temperature kit is mandatory.